Generate New Concept for Your Liquid ProductionGenerate New Concept for Your Liquid Production
Homogenizing & Emulsification SolutionsHomogenizing & Emulsification Solutions
Pharma & Cosmetic & Food Fluid ProcessingPharma & Cosmetic & Food Fluid Processing

Generate New Concept for Your Liquid Production

Innovative mixing and pumping technologies, inspiring the future of liquid processing.

Mixing & Blending Solutions
Hygienic Centrifugal Pumps: Ensuring Pure and Contamination-Free Transfer in Micellar Water Manufacturing

Optimize micellar water production with ASME BPE compliant hygienic centrifugal pumps. Eliminate biofilm with Ra<=0.4um EP finishes and open impellers.
Gentle Transfer Process for Cosmetic Emulsions and Active Raw Materials with Sine Pump

The final quality of cosmetic products depends entirely on stable formula structure and complete active ingredients after production. Any harsh conveying behavior during processing will compromise the texture, efficacy, appearance and shelf p...
Perfecting BB Cream Formulations: Pigment Dispersion Processes via a Batch High Shear Dispersing Emulsifier

Achieving a flawless color profile is the ultimate benchmark of a premium BB cream, liquid foundation, or tinted moisturizer. Unlike transparent skincare gels, color cosmetics rely on a precise balance of liquid emulsions and solid mineral powders—primarily titanium dioxide and iron oxides. The biggest nightmare for a cosmetics production manager is color drifting: when a batch formulated for a 'Light Beige' shade ends up looking streaky, chalky, or entirely different once applied to the skin.This critical quality failure stems from inadequate powder processing. Inorganic pigments are naturally hydrophobic and prone to clustering into stubborn micro-agglomerates. Traditional anchor mixers or low-shear stirrers merely push these powder lumps around the tank rather than breaking them down. This results in undispersed color specks and unstable shelf life.By integrating a Batch High Shear Dispersing Emulsifier directly into the core formulation line, factories can eliminate these formulation errors, ensuring flawless color payoff and long-term suspension stability.…
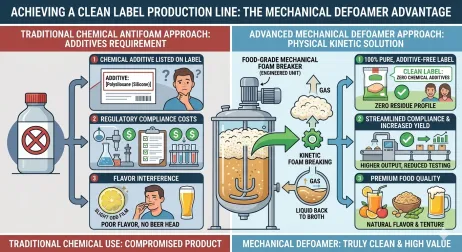
Food-Grade Mechanical Defoamers: Achieving a Clean Label Production Line

Support clean-label food production with food-grade mechanical defoamers that break foam, recover process liquid, and reduce reliance on chemical antifoam.

Applications
Meeting Strict GMP Standards: Hygienic Magnetic Pumps in Biopharmaceutical Manufacturing ProcessesIn the biopharmaceutical and life sciences sectors, the safety and purity of the end product dictate the survival of an enterprise. Whether manufacturing high-value monoclonal antibodies, recombinant proteins, novel vaccines, blood products, or formulating Water for Injection (WFI) and sterile buffers, these end products are administered directly into the human body for injection or clinical therapy. The end products of biopharmaceuticals have nearly draconian requirements for the production environment. Any microscopic bacterial growth, foreign mechanical particle contamination, or fluid leakage will directly force the disposal of an entire precious batch worth millions of dollars, or even trigger a severe regulatory compliance crisis. To satisfy the stringent GMP and FDA standards of international regulatory agencies, completely closed, leak-free sanitary magnetic drive pumps have become indispensable fluid equipment in downstream sterile pharmaceutical processing. 1. Eliminating Particle Contamination: Securing Absolute Purity of Sterile Liquids and WFI For end products such as injectables, vaccines, and blood products, insoluble particles represent a critical metric for quality control. Traditional fluid pumps mostly utilize dynamic seals, such as mechanical seals. During pump operation, the continuous friction between the dynamic and static rings inevitably generates microscopic mechanical wear debris, including carbon particles, graphite, or polymer flakes. Once mixed into the medicine, these particles not only destroy the clarity of the end product but can also clog expensive ultrafiltration membranes during subsequent sterile filtration stages. Sanitary magnetic pumps utilize shaft-seal-free magnetic coupling transmission technology, upgrading traditional dynamic shaft seals to a completely closed, static containment shell. The internal rotor and impeller spin entirely via non-contact magnetic force, fundamentally eliminating physical damage to the liquid from dynamic friction. This processing feature of zero mechanical wear particles perfectly aligns with the strict GMP requirement that sterile preparation manufacturing must not introduce foreign particles, ensuring the absolute purity of every batch of vaccine and liquid medicine leaving the factory. 2. Dead-Zone-Free and Electropolished Design: Preventing Biofilm Growth and Cross-Contamination Biopharmaceutical manufacturing belongs to a highly sensitive, biologically active environment where Active Pharmaceutical Ingredients (APIs) and finished products can easily become breeding grounds for bacteria and pyrogens. If dead zones with fluid stagnation exist inside the pump body, or if the surface is not smooth enough, residual medicine will form stubborn biofilms. This results in catastrophic microbial cross-contamination for subsequent product batches. Sanitary magnetic pumps designed specifically for pharmaceutical processes use high-specification 316L stainless steel for all wetted parts, treated with deep electropolishing to achieve a surface roughness of Ra <= 0.4 um. This extreme surface smoothness prevents cell suspensions or protein molecules from adhering. Furthermore, the pump features a completely open flow path and self-draining structure, guaranteeing that during Clean-in-Place (CIP) and Sterilization-in-Place (SIP) cycles, high-pressure steam and chemical cleaning solutions flush through and penetrate every single corner 100 percent. This dead-zone-free cleaning capability ensures zero residue and zero cross-contamination when multi-product facilities switch production between different batches of biopharmaceutical end products. 3. Gentle Hydraulic Shear: Preserving the Activity of Shear-Sensitive Biologics Many modern biological drugs, such as cell therapies, live virus vaccines, or long-chain proteins, are extremely sensitive to physical shear forces. If traditional pumping equipment features overly complex flow paths or excessive local velocities, high shear forces will directly rupture cell membranes or cause protein macromolecules to denature and deactivate, drastically reducing the active ingredient yield of the end product. Sanitary magnetic pumps utilize optimized semi-open impellers coupled with low-shear, low-velocity hydraulic engineering to provide extremely gentle and stable fluid dynamics during liquid transfer. This ensures that fragile biologically active ingredients maintain their original spatial structure and efficacy even after experiencing high-density pipe transfer, sterile filtration, and final filling processes, stably improving the overall production yield of the medicine. On multi-product biopharmaceutical lines, sanitary magnetic drive pumps are more than just fluid transfer machines, they are safeguards for end-product drug quality and GMP compliance. By virtue of their zero-leakage, particle-free, easily cleanable, and low-shear processing advantages, they defuse the core risks of biological products in sterile manufacturing from the very source. Choosing high-standard sanitary magnetic pumps is a critical initiative for pharmaceutical enterprises to demonstrate process reliability to regulatory authorities and protect patient safety.

Products

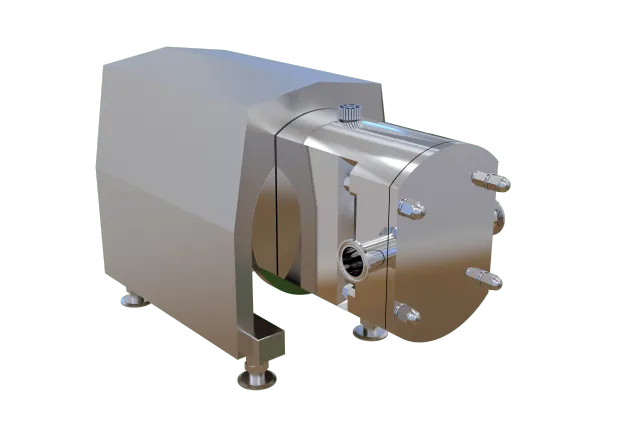
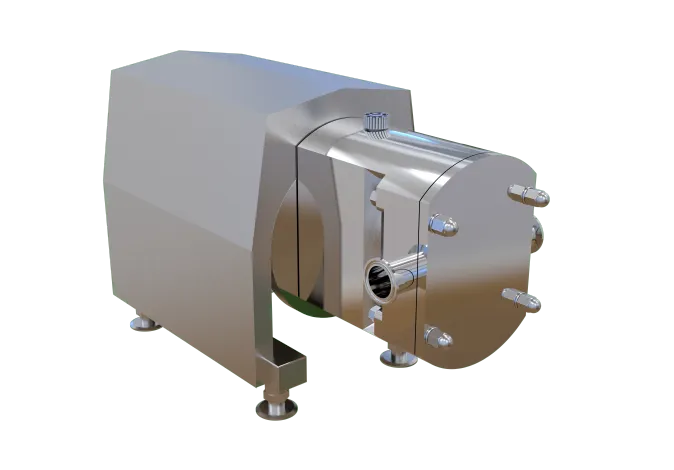
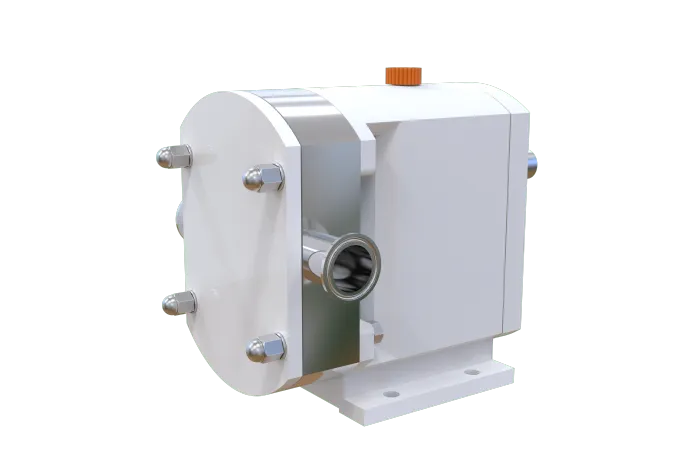
Close-Coupled Rotary Lobe Pump

Discover TRA sanitary rotary lobe pumps with integrated monoblock design. Certified by 3A and CE for high viscosity proc...
Baseplate Mounted Rotary Lobe Pump

Explore TR series modular split-frame rotary lobe pumps. Engineered with flexible shaft couplings and separate baseplate...
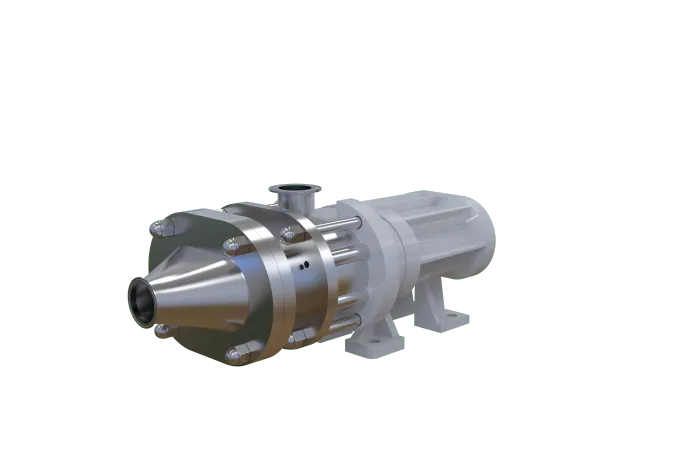
Sanitary Twin-Screw Pump

Explore sanitary twin-screw pumps for low-pulse fluid transfer, high-viscosity products, reversible operation, hygienic ...
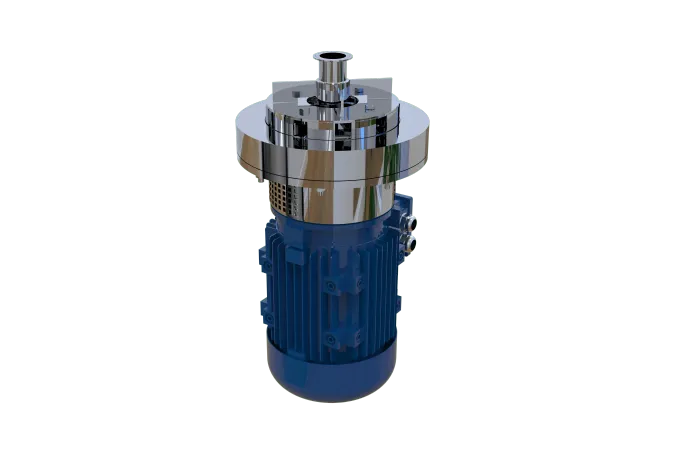
Fermenter Bottom Aerator

Explore DAWT bottom-mounted aerators for aerobic fermentation, combining air induction, gas-liquid mixing, and fine bubb...

Boao News

How to Choose a Top-Mounted Magnetic Agitator for a Stainless Steel Tank

2026-10-28

Learn how to select a top-mounted magnetic agitator for stainless steel tanks by evaluating mounting design, bearing materials, CIP/SIP compatibility, and torque requirements.
How to Select an Impeller for a Top-Mounted Magnetic Agitator

2026-10-28

Learn how to select the right impeller for a top-mounted magnetic agitator based on fluid viscosity, mixing objectives, vessel geometry, and process requirements.
What Determines the Torque Requirements of a Magnetic Agitator?

2026-10-28

Learn how liquid viscosity, impeller size, operating speed, solids loading, and startup conditions determine the torque requirements of a magnetic agitator.
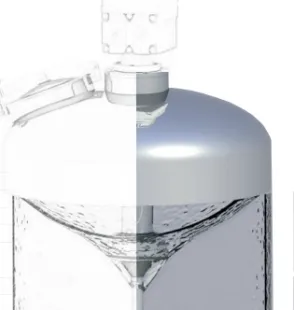
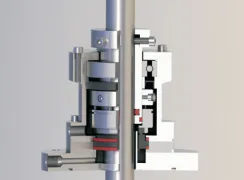
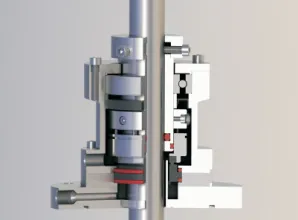
Magnetic Drive Mixer vs. Mechanical Seal Mixer: Maintenance and Operating Costs

2026-10-26

Compare magnetic drive and mechanical seal mixers in maintenance, leakage risk, downtime, and lifecycle costs to identify the right solution for industrial processing tanks.
About Us

With over two decades of expertise, Boao is a certified high-tech enterprise specializing in the R&D, design, and manufacturing of sanitary-grade mixing, homogenization, emulsification, and fluid systems. Our engineering team utilizes advanced CFD fluid simulations to optimize equipment performance, ensuring maximum operational efficiency and reliable quality. Driven by innovation, our facility features advanced processing and inspection equipment, including CNC machining centers, dynamic balancing testers, spectrometers, and coordinate measuring machines, allowing us to continuously refine products based on feedback from global users. Through years of patented R&D, Boao has become a preferred global supplier known for complete specifications, superior quality, and exceptional cost-effectiveness.

Partners
Why Choose US

Leading R&D and Continuous Innovation
Driven by a top-tier team and cutting-edge facilities, we continuously invest in advanced technology to deliver market-leading products that keep your business ahead of the competition.

Efficient Operations and Reliable Supply Chain

Our smart, automated production systems maximize efficiency, while our robust supply chain partnerships guarantee stable product quality and on-time delivery.

Global Footprint and Trusted Brand Influence

With a strong domestic and international presence, our brand has earned the trust of countless global clients through proven quality and consistent market recognition.

Comprehensive End to End Customer Support

We offer a seamless one stop service from pre sales consultation to after sales support to ensure prompt solutions and maximize value for your business.

Top Talent and Continuous Growth

Our highly skilled professional team stays ahead of industry trends through ongoing training, fueling our innovation and providing expert support for your projects.